High-Purity Botanical Extracts & Standardized Fruit Ingredients
In addition to industrial banana fruit bases and specialty dietary fiber fractions, UniCare delivers certified botanical active ingredients verified batch-by-batch via chromatographic fingerprinting.
-
 China Rhodiola Rosea Extract Suppliers, Factory
Rhodiola Rosea Extract
Standardized Salidroside 1%-5% & Rosavins 3% by HPLC for metabolic and adaptogenic formulation compliance.
-
 Wholesale Pomegranate Extract Suppliers, Factory
Pomegranate Extract
Ellagic Acid 40%-90% and Punicalagins 30%-40% for cellular oxidative defense and functional food pigmentation.
-
 China Quercetin Suppliers, Factories
Quercetin Dihydrate 95%-98%
HPLC-verified flavonoid derived from Sophora japonica, compliant with USP/EP heavy metal and residue specs.
-
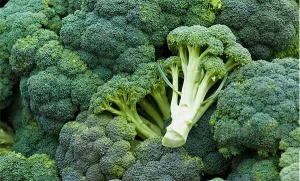 China Broccoli Seed Extract Factories, Exporter
Broccoli Seed Extract
Standardized Glucoraphanin 1% to 20% by HPLC, pre-cursor to sulforaphane for phase II detoxification pathways.
-
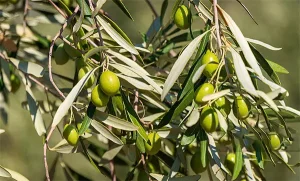 Best Olive Leaf Extract Exporter, Exporters
Olive Leaf Extract
Standardized Oleuropein 20%-40% and Hydroxytyrosol for cardiovascular support and antioxidant formulations.
-
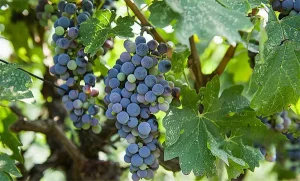 Best Grape Seed Extract (GSE) Supplier, Factory
Grape Seed Extract (GSE)
Standardized Proanthocyanidins (OPC) 95% by UV/HPLC, premium polyphenol grade for nutraceutical formulations.
-
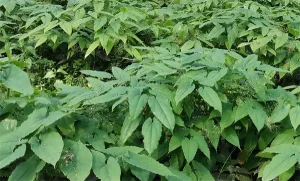 Wholesale Epimedium Extract Suppliers, Factory
Epimedium Extract (Icariin)
Purified active fractions from 10% to 98% Icariin, manufactured under strict continuous countercurrent extraction.
-
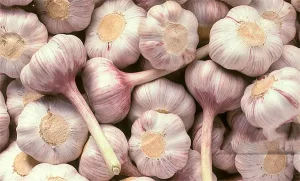 Best Garlic Extract Factory, Exporter
Garlic Extract (Allicin)
Odor-controlled standardized Alliin and Allicin yield for heart health formulations, tested by gas chromatography.
The Global Banana Agro-Industrial Trade & Commercial Landscape
A multi-billion dollar shift from perishable commodity logistics to bio-refined functional ingredients, climate-resilient cultivars, and integrated global supply ecosystems.
135+ MT Macro Production Scale
The global production of bananas (*Musa acuminata* and hybrid cultivars) exceeds 135 million metric tons annually, anchoring agricultural GDP across tropical zones in Ecuador, the Philippines, Guatemala, Colombia, and southern China. While the fresh table fruit export trade generates upwards of $14.5 billion, post-harvest losses historically reached 25-30% due to narrow maturation windows and supply-demand imbalances.
Global Trade MetricsThe Industrial Bio-Refining Transition
Procurement teams are progressively migrating from basic purees toward high-value, standardized functional fractions. Modern industrial processors isolate Type II Resistant Starch (RS2), unripened green banana flours, enzymatically clarified spray-dried instant powders, and polyphenol-dense banana peel extracts that serve dietary supplement, sports nutrition, and clean-label bakery applications.
Functional Value CreationFusarium Wilt (TR4) Resilience
The agronomic hegemony of the Cavendish monoculture faces unprecedented vulnerability from *Fusarium oxysporum* f. sp. *cubense* Tropical Race 4 (TR4). Elite global suppliers and exporters are partnering with bio-tech breeding stations to deploy micropropagation tissue culture, gene-edited cultivars, and diversified agroforestry models to ensure continuous, non-disrupted raw material availability.
Supply Continuity ProtocolsEngineering Banana Bio-Fractions: Resistant Starch, Enzymes & Flavour Powders
From unripened stage-1 green fruit to ripened stage-6 spray-dried purees, our controlled industrial extraction matrix stabilizes native bioactives without thermal degradation.
Green Banana RS2 Starch
Derived exclusively from stage 1-2 unripened bananas where starch crystallization remains intact. Utilizing continuous low-temperature wet milling and flash drying under 55°C, the native B-type semicrystalline polymorph is preserved. This yields over 60% resistant starch (RS2), providing an ideal prebiotic substrate that ferments into butyrate in the distal colon without elevating glycemic index.
Prebiotic & Glycemic RegulationFlash Spray-Dried Instant Powders
Engineered from Stage 5-6 fully ripened fruit where natural sucrose, fructose, and aromatic esters peak. In-line centrifugal enzymatic de-pectinization reduces molecular viscosity before feed-stock atomization in a countercurrent drying chamber. Operating at precisely regulated inlet/outlet temperatures (165°C/78°C), native volatile isoamyl acetate compounds are encapsulated, eliminating burnt off-notes.
Flavor & Rapid RehydrationBioactive Peel Polyphenols
Utilizing high-pressure green solvent extraction, secondary agricultural co-products (banana exocarp) are processed to extract concentrated gallocatechin, dopamine precursors, and carotenoids (lutein and β-carotene). Tested by Agilent UHPLC, these botanical extracts provide substantial DPPH free-radical scavenging capacity for nutraceutical and cosmetic dermo-protective formulations.
Zero-Waste Upcycling| Commercial Grade | Maturation Phase | Primary Active / Marker | Moisture (%) | Analytical Method | Standard Packaging |
|---|---|---|---|---|---|
| Functional Green Banana Powder | Stage 1 (Unripened, Peel Green) | Resistant Starch ≥ 60.0% | ≤ 6.0% | AOAC 2002.02 / HPLC | 25 kg Multi-ply Kraft Drum |
| Spray-Dried Ripe Banana Powder | Stage 6 (Fully Yellow, Brix ≥ 21°) | Natural Fructose/Glucose ≥ 45% | ≤ 4.0% | HPLC Carbohydrate Panel | 20 kg Vacuum Aluminum Bag |
| Freeze-Dried (FD) Banana Dices/Powder | Stage 5 (Yellow with Green Tip) | Pulp Integrity ≥ 98%, Vitamin B6 | ≤ 2.5% | Karl Fischer Titration | 10 kg Nitrogen-flushed Carton |
| Aseptic Clarified Banana Puree | Stage 6 (De-aerated, Flash Pasteurized) | Total Soluble Solids 22-24° Brix | N/A (Liquid) | Refractometry / pH Meter | 220 kg Aseptic Bag-in-Drum |
Precision Temperature Control, Controlled Atmosphere (CA) & Global Shipping
Eliminating chilling injuries and pre-mature ripening during trans-oceanic transit through real-time IoT monitoring and modified atmospheric equilibrium.
Thermal Window: 13.2°C – 14.0°C
Cavendish and plantain varieties suffer irreversible physiological chilling injury if subjected to pulp temperatures below 12.8°C (characterized by sub-epidermal vascular browning, lack of aroma development, and incomplete starch conversion). Our reefers maintain continuous air delivery within a tight ±0.3°C variance.
Critical Thermal ThresholdCA Regulation: O₂ & CO₂ Management
To put harvested green fruit into vegetative dormancy during 20 to 35-day oceanic voyages, reefer containers employ active Controlled Atmosphere technology: lowering Oxygen (O₂) to 2%-5% and elevating Carbon Dioxide (CO₂) to 3%-5%. This slows respiration rates and delays climacteric ethylene triggering.
Atmospheric EquilibriumCatalytic Ethylene Scrubbing
Ethylene (C₂H₄) in concentrations as dilute as 0.05 ppm initiates rapid endogenous senescence. Export loads are protected via integrated potassium permanganate (KMnO₄) scrubbing filters and ozone-assisted catalytic oxidation systems, neutralizing airborne phytohormones across long-haul marine corridors.
Senescence PreventionLive Telemetry & Phytosanitary Tracking
Every maritime container is fitted with autonomous satellite-linked IoT sensors reporting core pulp temperature, ambient relative humidity (maintained at 90-95% to avoid fruit dehydration), O₂/CO₂ partial pressures, and GPS coordinates directly to enterprise procurement portals in real time.
Global IoT VisibilityCross-Industry Application Scenarios for Food, Pharma & Nutraceuticals
Examining technical formulation methodologies, synergy with botanical actives, and processing behavior across diverse commercial end-user environments.
Clean-Label & Gluten-Free Bakery
Challenge: Replacing wheat flour without compromising crumb elasticity or inducing glycemic spikes.
Engineering Solution: Green Banana Resistant Starch (RS2) acts as a functional hydrocolloid. With an amylose-to-amylopectin ratio of ~30:70, it binds free moisture, delays starch retrogradation (extending shelf-life by 48 hours), and provides an EFSA/FDA-compliant prebiotic fiber claim while reducing net formulation carbohydrates by 22%.
Sports Performance & Hypotonic Hydration
Challenge: Formulating an instant-dissolving natural electrolyte matrix without synthetic potassium chloride off-notes.
Engineering Solution: Spray-Dried Ripe Banana Powder provides 1,200mg+ bioavailable potassium per 100g, bound to native malic and citric organic acids. Blended synergistically with UniCare's Grape Seed Extract (GSE) and Quercetin, the compound supports nitric-oxide mediated vasodilation and accelerated post-exercise glycogen replenishment.
Microbiome & Clinical Enteral Nutrition
Challenge: Providing non-irritating, non-bloating gut nourishment in medical meal replacements.
Engineering Solution: Green banana starch passes unhydrolyzed through the upper GI tract into the caecum. Microbiota fermentation elevates intestinal short-chain fatty acids (primarily acetate, propionate, and butyrate), lowering colonic luminal pH and reinforcing tight junction proteins (Claudin-1, Occludin) to mitigate mucosal gut barrier leakage.
Batch-Specific Verification: Chromatographic Purity, Safety & Certifications
Our collaborative manufacturing hubs operate under ISO 9001, ISO 22000, HACCP, GMP, and EU-GMP frameworks, deploying multi-platform analytical instruments for uncompromising batch qualification.
Chromatography Suite
Partner quality control centers house 2× Agilent 1290 UHPLC, 4× Agilent 1260 HPLC, 2× Shimadzu LC-20AT HPLC, and 2× Dionex HPLC units. Active constituents, organic acids, and polyphenol marker compounds are verified against USP reference standards prior to commercial batch release.
Assay PotencyMass Spectrometry & GC
Equipped with Shimadzu GC2010 gas chromatography and GC-MS/MS systems to verify solvent recovery limits and screen for over 450 agricultural pesticide residues (including organochlorines and organophosphates) well beneath stringent European Regulation (EC) No 396/2005 limits.
Trace Contaminant ScreenICP-MS Heavy Metals
Utilizing Inductively Coupled Plasma Mass Spectrometry (ICP-MS), every manufactured lot is screened for toxic elemental accumulation: Lead (Pb < 0.5 ppm), Arsenic (As < 0.5 ppm), Cadmium (Cd < 0.1 ppm), and Mercury (Hg < 0.05 ppm), ensuring complete safety for infant and clinical nutrition.
Elemental PurityMicrobiological Assurance
Batch tests confirm absent *Salmonella* spp. (in 25g), zero *Escherichia coli*, negative *Listeria monocytogenes*, with total aerobic microbial counts (TAMC ≤ 1,000 CFU/g) and total yeast/mold counts (TYMC ≤ 100 CFU/g) compliant with British and US Pharmacopeial microbiological thresholds.
Bio-Safety ControlTechnology Roadmap: Precision Agriculture, Green Solvents & Circular Bio-Economy
Anticipating structural supply chain transformations and developing next-generation bio-refining architectures to ensure sustainable, resilient global trade.
CRISPR-Cas9 & TR4 Bio-Defenses
Over the next decade, genomic engineering is introducing site-directed mutations into Cavendish RGA2 receptors and silencing susceptibility genes to confer endogenous immunity against Tropical Race 4 wilt. This eliminates chemical soil fumigants, stabilises annual yields, and ensures long-term crop continuity without altering the nutritional composition of harvested bananas.
Phase: Field Validation (2025-2028)Supercritical & Subcritical Extraction
Phasing out conventional organic extraction solvents in favor of Supercritical Fluid CO₂ (scCO₂) and subcritical pressurized hot water (PHW) processing. This allows non-thermal fractionation of aromatic esters, banana waxes, and peel antioxidants without residual solvent traces, reducing carbon expenditure by up to 35% across processing plants.
Phase: Industrial Rollout (2026-2030)Pseudostem Cellulose Valorization
Pioneering closed-loop agricultural processing by transforming discarded banana pseudostem fibers into high-tensile microcrystalline cellulose (MCC), compostable agricultural mulching films, and biodegradable inner lining for our bulk export shipping cartons, replacing petroleum-derived plastics across maritime transit.
Phase: Scale Production (2028-2035)Frequently Answered Qualification Questions for International Buyers
Essential regulatory, analytical, logistics, and supply parameters required by quality assurance, R&D, and procurement executives.
What are the exact minimum order quantities (MOQ) and packaging formats for fresh export and processed powders?
How is Resistant Starch (RS2) content standardized and verified across harvest batches?
What certifications accompany commercial shipments to North America, the European Union, and Asia-Pacific?
How do your cold-chain logistics mitigate premature ripening and crown rot during transit?
Can UniCare customize fruit powder particle size, moisture profiles, or botanical blends?
What are the lead times for industrial supply contracts and spot sample evaluations?
High-Performance Functional Extracts for B2B Supplement & Beverage Brands
Manufactured under continuous countercurrent extraction to provide rock-solid batch reproducibility, low microbial burdens, and fully traceable origin dossiers.
-
China Quercetin Suppliers, Factories
China Quercetin Suppliers
95% & 98% HPLC purity, low bio-contaminant profile, ideal for cellular health, cardiovascular, and respiratory formulas.
-
China Broccoli Seed Extract Factories, Exporter
China Broccoli Seed Extract
High glucoraphanin yield verified by HPLC, supporting clinical Phase II enzyme induction and cellular detox.
-
Best Olive Leaf Extract Exporter, Exporters
Best Olive Leaf Extract
Standardized Oleuropein and polyphenol fractions for metabolic optimization and blood lipid balance.
-
Best Grape Seed Extract (GSE) Supplier, Factory
Best Grape Seed Extract (GSE)
OPC 95% minimum by UV/HPLC, solvent-residue compliant for international functional beverage markets.
-
Wholesale Epimedium Extract Suppliers, Factory
Wholesale Epimedium Extract
Precise Icariin specs (10%-98%) tested via Dionex HPLC, validated for vitality and sports formulation lines.
-
Best Garlic Extract Factory, Exporter
Best Garlic Extract Factory
Potent Alliin / Allicin active content, deodorized fine powder for capsules, tablets, and functional blends.
-
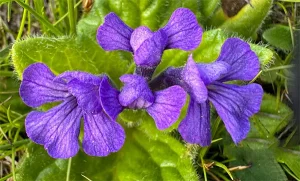 Best Ajuga Extract Suppliers, Exporters
Best Ajuga Extract
Standardized Turkesterone 2% to 10% HPLC for high-potency sports nutrition and muscle protein synthesis formulas.
-
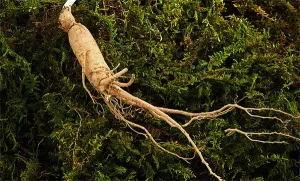 Best Ginseng Extract Suppliers, Factories
Best Ginseng Extract Suppliers
Standardized Panax Ginsenosides 10% to 80% UV/HPLC for cognitive stamina, immune vitality, and tonics.
Initiate Your Supplier Qualification & Sample Dossier
Partner with an authoritative agricultural and botanical active ingredient exporter. Request complete technical data packages, batch-specific Certificates of Analysis (COA), or customized pilot sample shipments.